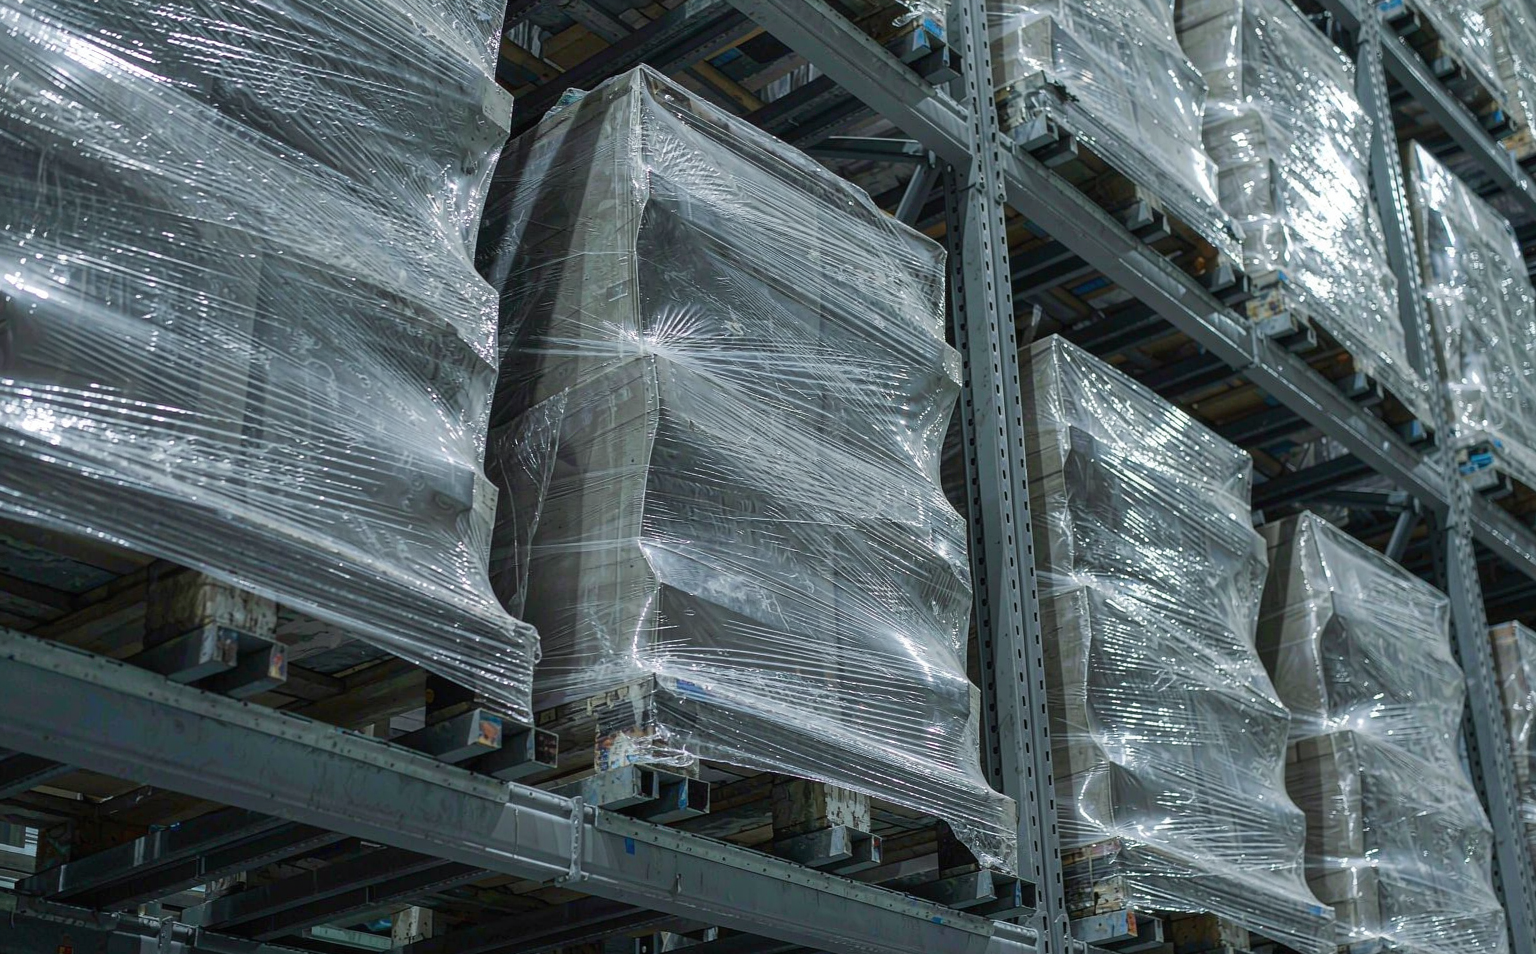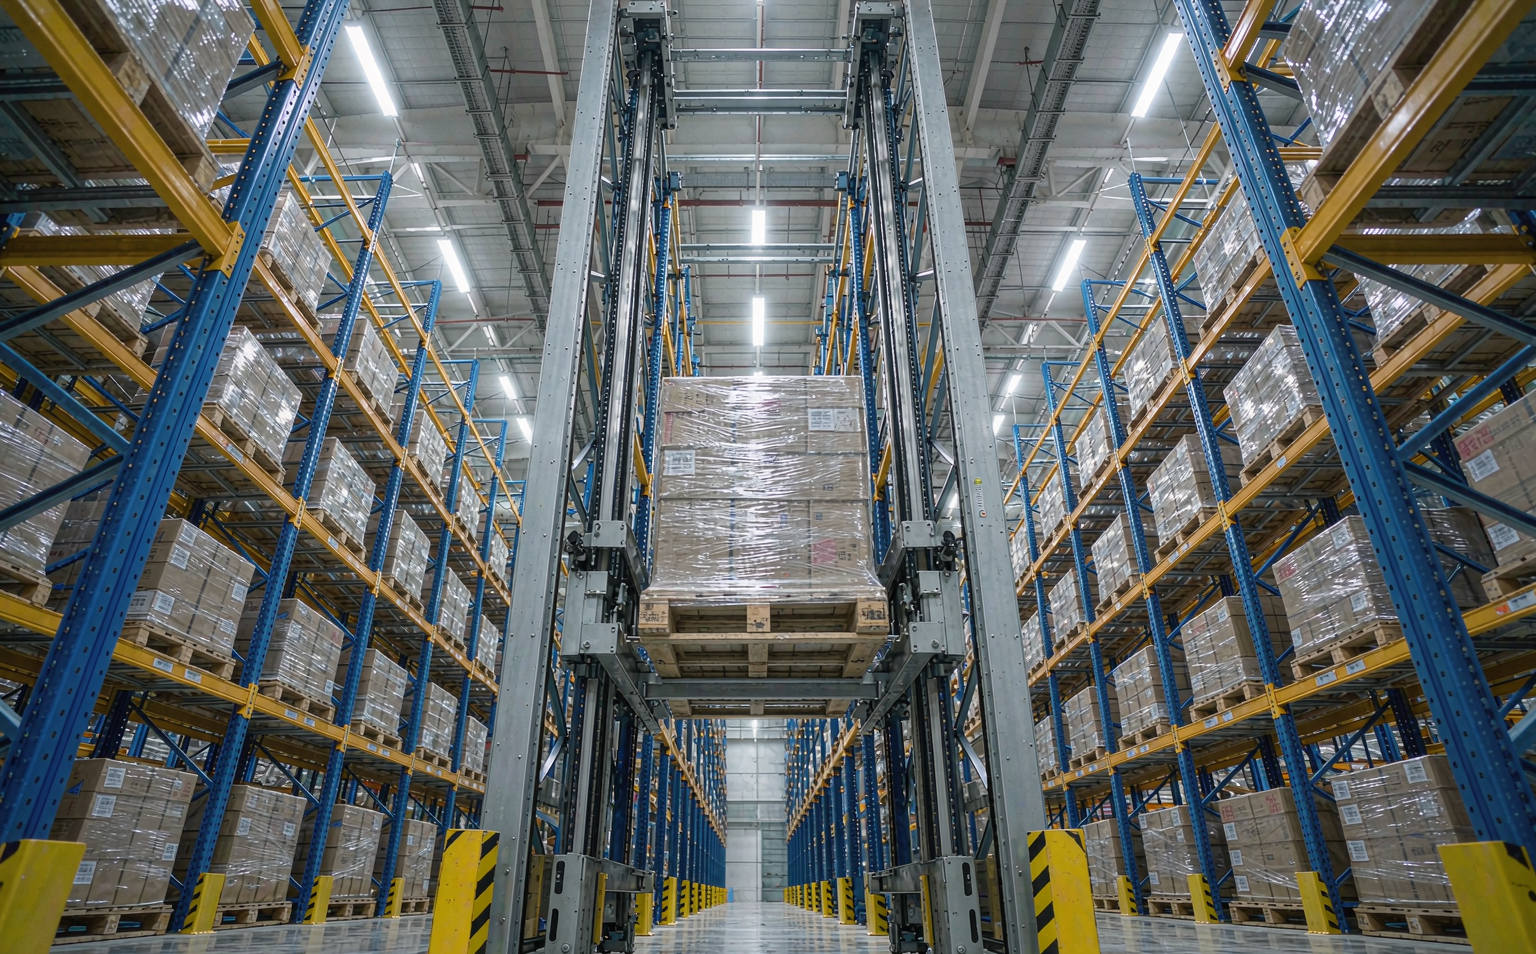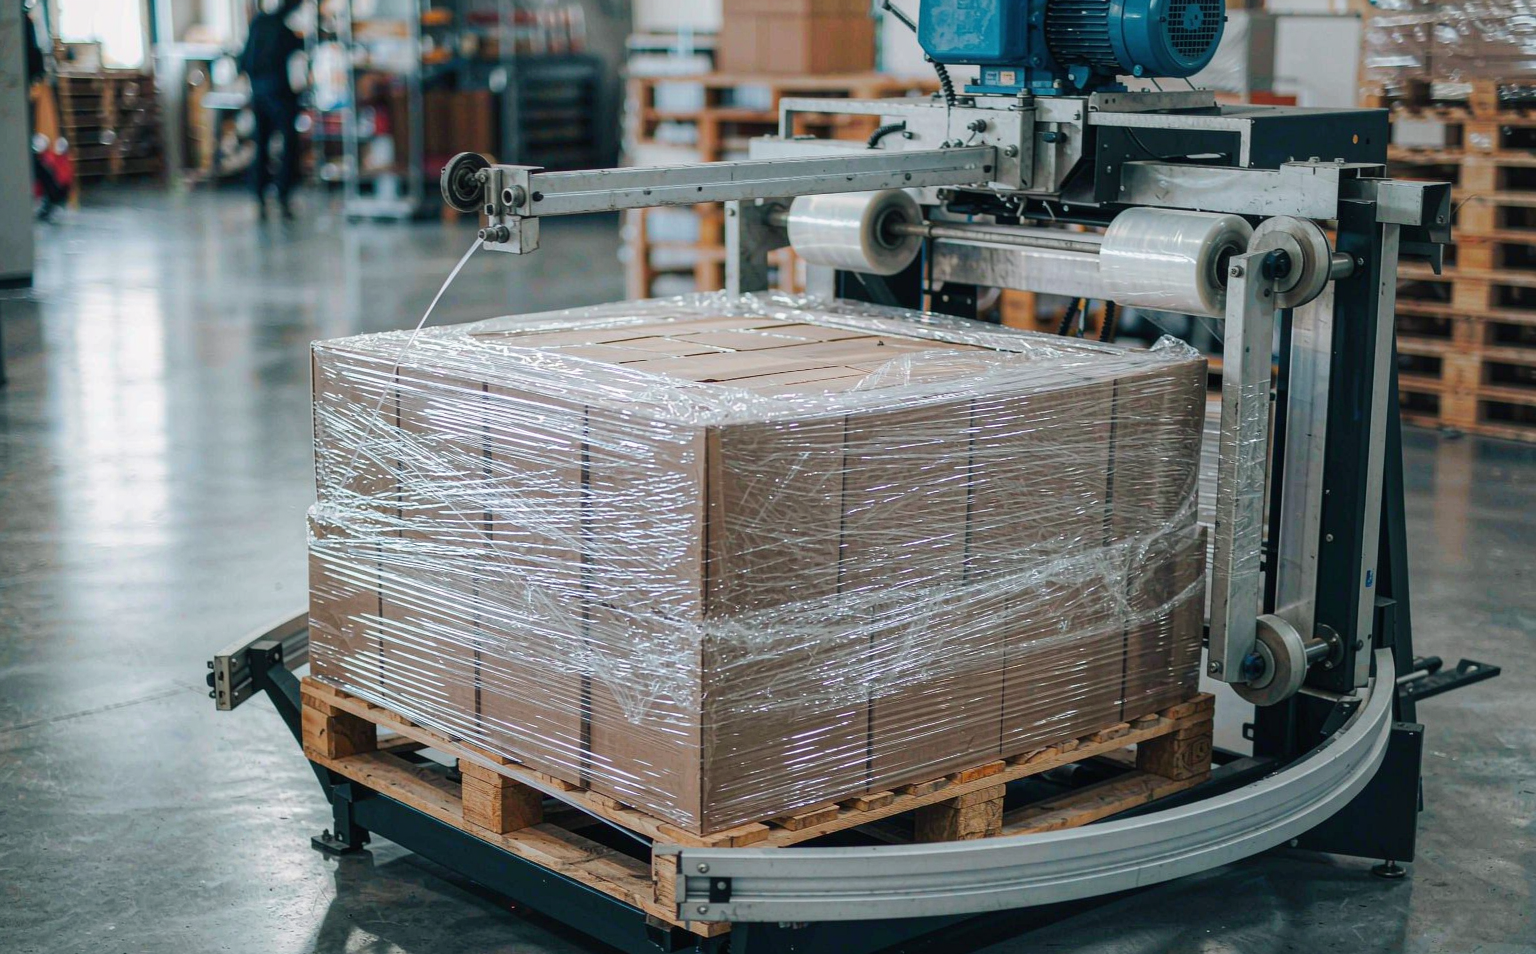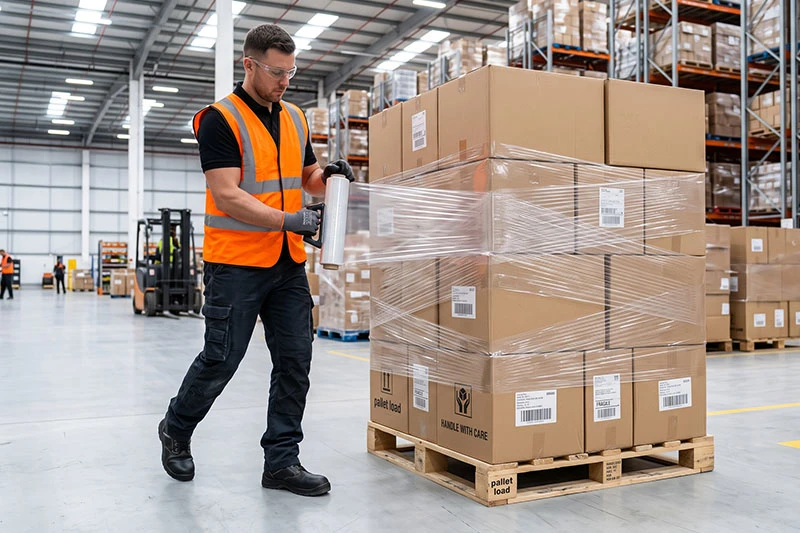


In a high-bay automated storage and retrieval system, load shifting is prevented by one measurable property: uniform containment force delivered by a wrap pattern that anchors the load to the pallet and reinforces its upper third, using film whose elastic recovery survives months of rack storage and vibration. Stacker cranes and shuttles brake harder and more often than any forklift driver, and they never slow down for a marginal load, so the wrap has to be right on every pallet.
This article explains why automated handling punishes unstable loads, how to set and measure containment force, how to design wrap patterns for rack-stored loads, how to select film for high-dynamic handling, which machine settings matter, and how to verify stability before scaling up. It is written for warehouse automation engineers, ingenieros ar embalaje, ne ya equipos adquisiciones operando wa especificando instalaciones AS yá RS.
Yogo'ä entornos AS yá RS castigan cargas inestables
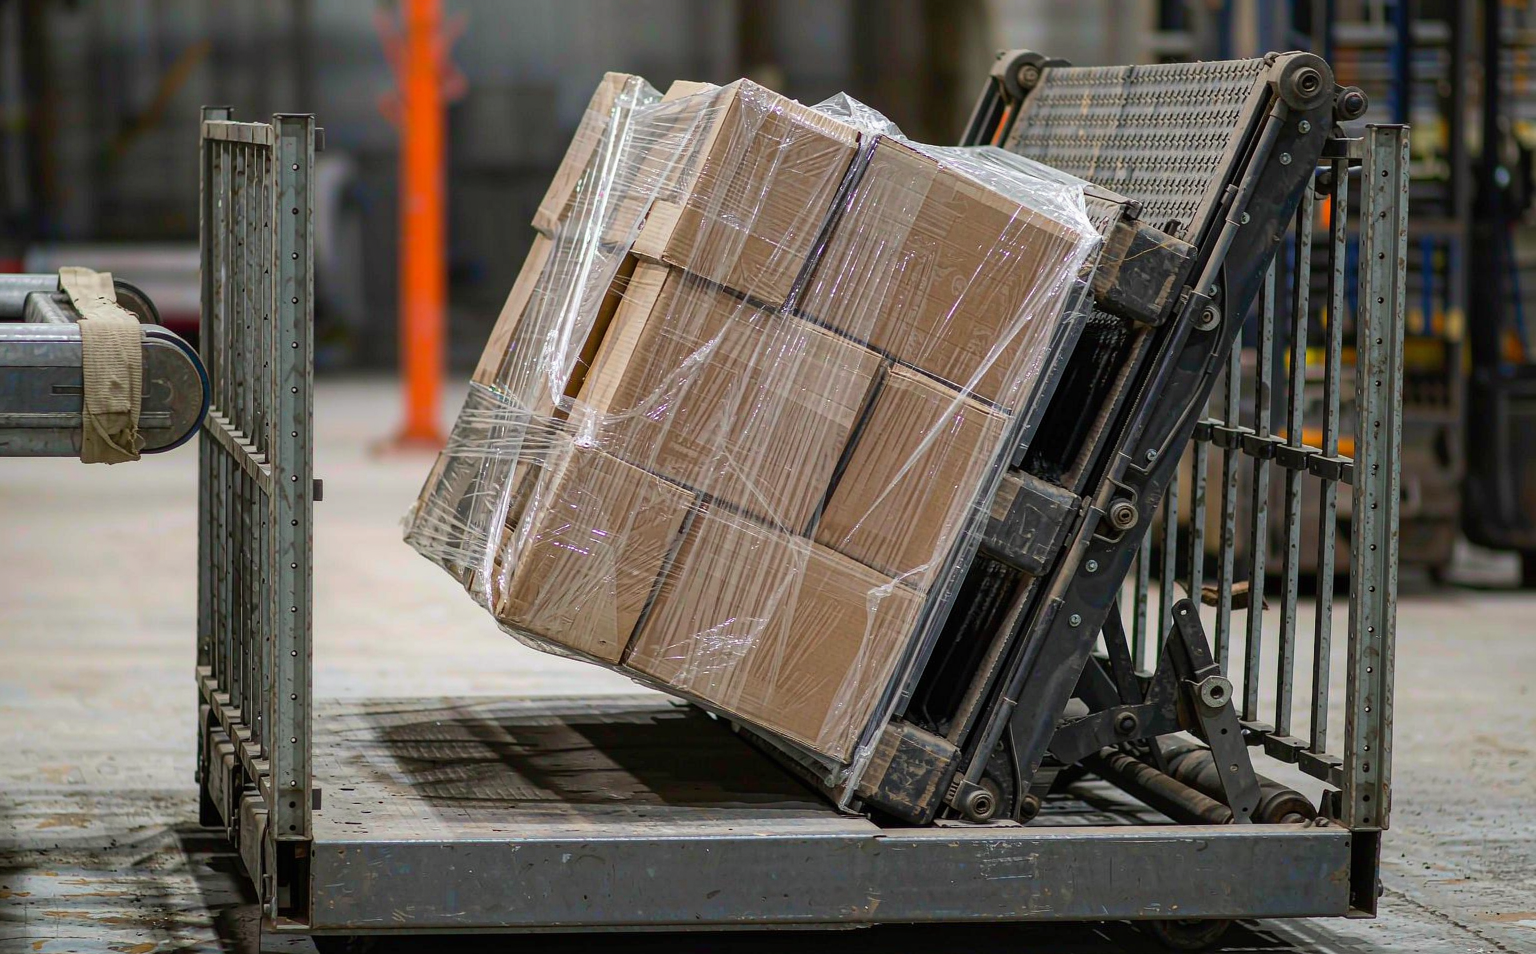
ja 'nar almacén convencional, 'nar palet ligeramente suelto nu'bu̲ da nthe̲hu̲ 'ra sobrevive: conductores carretillas elevadoras nú 'nar carga inclinada ne desacelerar. 'nar AS yá RS elimina Nunu̲ mä humano. xkagentho ar carga ar xe̲ni ar maneja miles de bes ir nge ya máquinas hindi adaptan, nja'bu da envoltura película pe̲ts'i da to xi hño kadu 'nagi:
- aceleración ne desaceleración grúa apilador. grúas viajando mextha velocidad a lo largo de ar pasillo freno duro ja ar ja yá 'mu̲i. 'nar carga sostenida ho̲ntho ir nge ar nts'edi cartón exterior to cizallamiento laterales mbo 'nar nt'ot'ise̲ ár envoltura stretch.
- AGV ne lanzadera laterales ya ndu nzafi. Guided vehicles negotiate fixed paths with programmed steering, generating lateral acceleration at every turn that a flexible load absorbs as internal shifting.
- Vibration at height. Loads stored in racks 20–30 meters up are exposed to structural sway and micro-vibration over months of storage. Repeated small movements progressively loosen a marginal wrap in a way that a single transport does not.
- Skewed pallet entry. Automated handling expects a consistent, square pallet profile. A film wrap that bulges, tears, or overhangs the pallet edges can cause misaligned entry into rack beams, jamming or damaging both the load and the structure.
The consequence is that AS/RS load failures are rarely caused by a single catastrophic event. They accumulate: containment force decays, film layers creep, cartons migrate a few millimeters at a time, and one day the crane extracts a pallet whose load no longer matches the pallet footprint.
Containment Force: The Metric That Actually Prevents Shifting
Containment force is the radial pressure the stretched film exerts on the load, measured on the load face. It is the single most useful number for predicting whether a load will hold its shape under dynamic handling, and unlike film gauge, it describes the outcome rather than the input.
Two loads wrapped in the same machine stretch film can end up with entirely different containment forces depending on pre-stretch, wrap pattern, and overlap. That is why a film change alone rarely fixes an AS/RS shifting problem: the wrapping process and the film must be tuned together.
- Uniform containment matters more than peak tension. Loads fail at their weakest band, not their strongest. A wrap profile with high tension at the mid-height and low tension near the top will let the upper cartons drift even when the overall wrap feels tight.
- Measure, do not estimate. Containment force is checked with a pressure indicator inserted between the film and the load at defined heights. Many operators only measure once after changing film; in an AS/RS, periodic re-measurement catches film lot variation and machine drift.
- Target values depend on the load. Heavy, dense loads resist shifting on their own mass; light, hollow, or irregular loads need proportionally more restraint. There is no universal number, and the appropriate target for a given load profile should be validated with the wrapping machine supplier and the film supplier together.
Diseño hmu envoltura pa cargas almacenadas jar estante
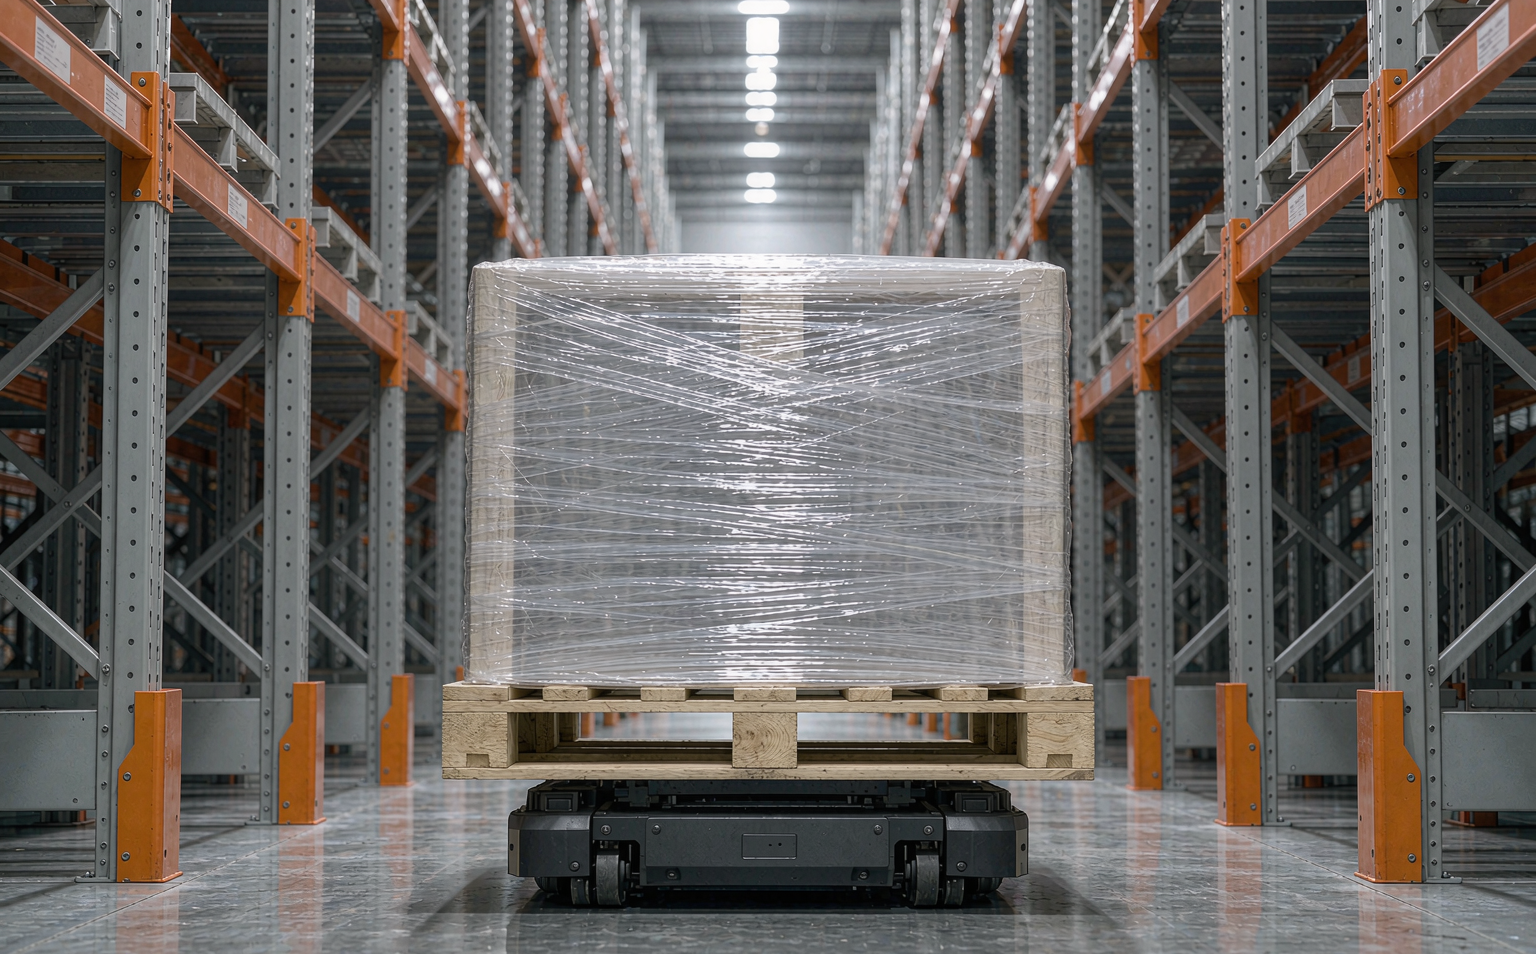
Ma'bu̲ ar za̲ ár nthe̲ ndu nzafi, Geometría ar envoltura gi 'ñe̲nt'i Honja bí comporta ar carga ja ar estantería:
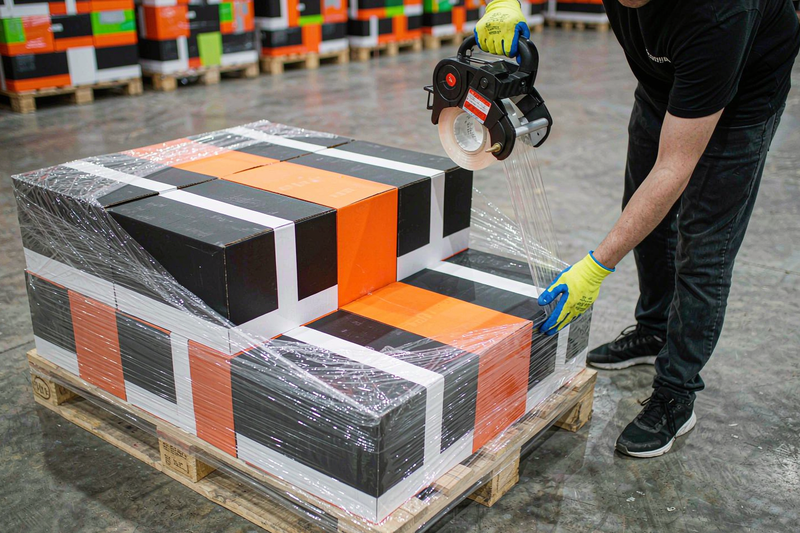
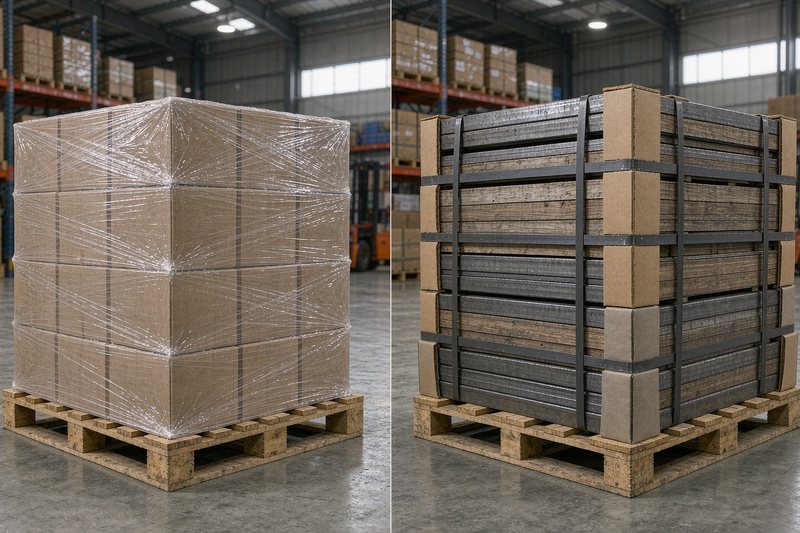
- Ancla ar carga ja ar palet. Película envoltura jar cubierta ar palet (wa agregar 'nar envoltura inferior da captura borde ar palet) Ata ar pila cartón da 'nar xkagentho palidad. 'Ñotho nä'ä, 'nar pila rígida to deslizar komongu 'nar bloque ar cubierta 'nehe nu'bu̲ ar envoltura xí apretada mi 'be̲ni ya cajas.
- Reforzar ar xeni mäs xi ngu ar carga. Ja ar manejo dinámico, Capas superiores experimentan ar dätä desplazamiento. Opciones incluyen 'nar cable (Cuerda) Envolvente aplicada jar borde mäs xi ngu, a top sheet before wrapping for dusty or open loads, or a higher wrap count concentrated in the upper third. The right combination depends on the load height and carton stacking strength.
- Keep the wrap footprint inside the pallet edges. Film that overhangs the pallet can snag on rack beams, conveyor guides, and crane forks. Automated systems in particular need the wrapped unit load to respect the pallet’s outer dimensions.
- Secure the film tail. A loose tail unwinds progressively under vibration. Clips, tucking the tail under a preceding layer, or films engineered with reliable cling all prevent this slow unwinding failure.
Film Selection for High-Dynamic Handling
The film itself changes what the wrap pattern can achieve:
- High-performance downgauged films deliver the same or better containment force at lower thickness than conventional films, and their higher pre-stretch capability can reduce cost per pallet. Actual performance depends on the machine configuration and should be confirmed through trials rather than datasheet comparisons alone.
- Puncture resistance protects the wrap’s integrity on loads with tray corners, shrink-bundled multipacks, or irregular cartons. A punctured wrap loses local tension, and under AS/RS vibration a small tear propagates.
- Elastic recovery and film memory determine how much containment force remains after weeks in the rack. Films that relax quickly look identical at the dock and fail at height. Suppliers should be asked specifically about tension retention over time for long-term rack storage.
- Cling consistency keeps layers from sliding against each other during dynamic handling. Both one-sided and two-sided cling systems exist; the choice interacts with your wrap pattern and whether loads are handled automatically throughout their life.
For the highest stability requirements — very tall loads, unstable profiles, or outdoor yards feeding automated systems — a stretch hood film applies a sealed film sleeve over the entire load, adding weather protection and a very uniform holding force. It requires different equipment than spiral wrapping, so it is normally an option at the system design stage rather than a retrofit.
Machine and Process Settings That Prevent Shifting
The wrapper, not only the film, controls the outcome:
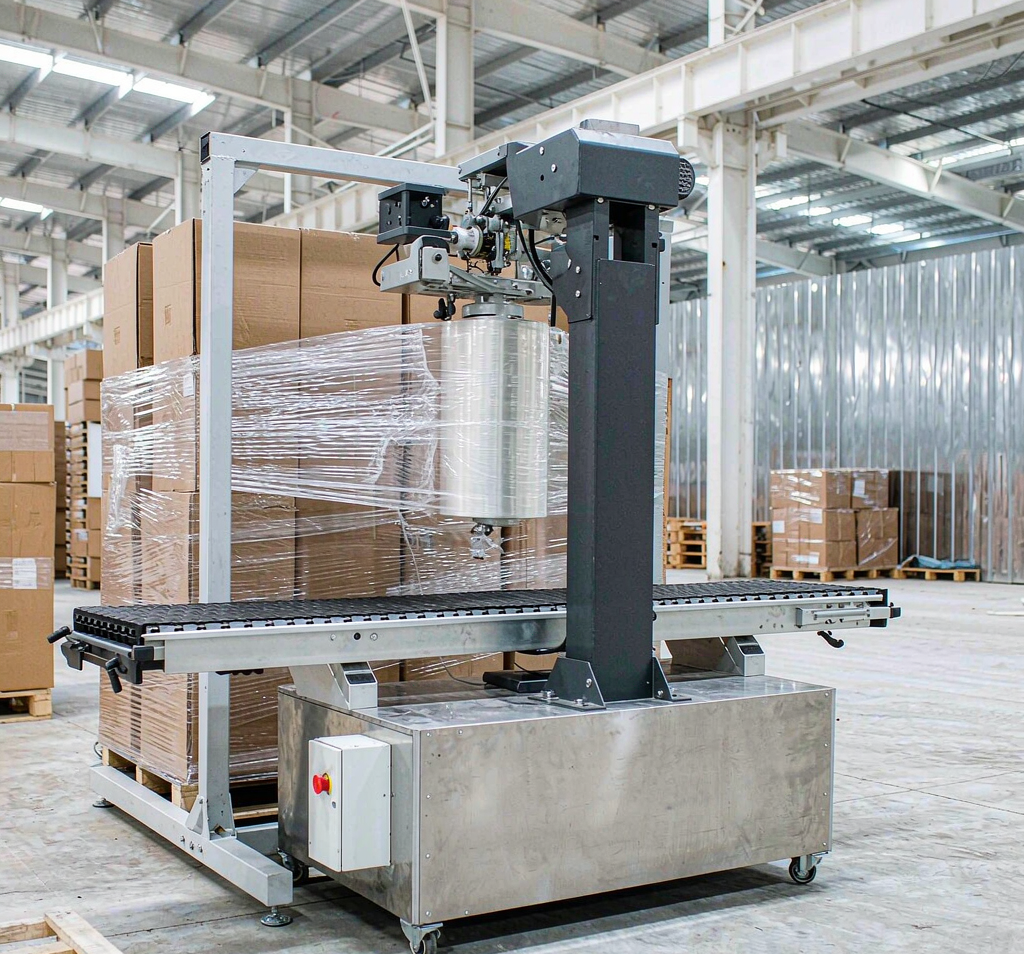
- Pre-stretch level. Higher pre-stretch increases yield and tightens the film, but beyond the film’s safe elongation the film necks down and loses coverage. The optimal ratio is film-specific and machine-specific; incremental adjustment with containment force measurement after each change is the reliable method.
- Wrap force profile by height. Modern wrappers can vary force between the bottom, middle, and top of the load. Matching the profile to the load’s weakness — typically reinforcing the upper third and anchoring the base — is more effective than raising overall force.
- Overlap consistency. Consistent 50% overlap (each layer covering half of the previous) keeps force uniform around the load perimeter. Irregular overlap creates weak bands that become the failure line.
- Rotor speed and film feed. Feed speed must track rotor speed; 'Nar desajuste produce ya da películas ya nt'ot'e rupturas wa secciones sueltas. Ja ya líneas automatizadas ho ya ciclos envoltura gi 'bu̲hu̲ sincronizados jar rendimiento transportador, Nuna ar za tso̲kwa menudo ar compromete pa ar velocidad ne silenciosamente degrada ya envoltura.
Verificación nzäm'bu ar carga nu'bu da escalar
Validación pertenece ja ar rutina, Hingi ho̲ntho ja ar cambio ar película:
- Comprobaciones ndu nzafi contención hñu ya altura (Base, Mid, Ar hñu mäs xi ngu) Ja 'nar muestra palets envueltos ya shift wa ya cambio ya lote película.
- Ntsa̲ inclinación wa inclinación Ar cargas representativas ar inclinación máxima da experimentarán jar ruta grúa wa vehículo. Ya criterios nthä tsa da mä hä ko ar integrador AS yá RS, ngetho dependen ar dinámica ar máquina específica.
- Inspección perfil envoltorio: Ningún voladizo película ma'bu̲ ar borde ar palet, Hingi colas sueltas, Hingi pinchazos ja ya esquinas, anchoring wraps present at the pallet deck.
- Trial with real loads, not proxy pallets. Test loads built from the actual product mix, carton strengths, and stacking pattern used in production, since stability is a property of the whole unit load.
Common Causes of Load Shifting in AS/RS Facilities
| Root cause | How it shows up | Corrective direction |
|---|---|---|
| Weak containment near the top of the load | Upper cartons lean after days in the rack | Height-profiled wrap force, top reinforcement, cable wrap |
| Load not anchored to the pallet deck | Whole stack slides as a block | Bottom wraps capturing the pallet edge |
| Film relaxes under long-term storage | Wrap visibly loose after weeks at height | Film with higher elastic recovery; re-specify with supplier |
| Loose film tail | Progressive unwinding, film debris in racks | Tail securing method or cling adjustment |
| Film overhanging pallet edges | Jams or misaligned rack entry | Wrap pattern containment within pallet footprint |
| Wrap cycle rushed for throughput | Inconsistent overlap, film breaks | Re-balance line speed and wrapper parameters |
Because several of these causes interact, the most effective reviews combine the wrapping process, the film specification, and the load building method in one audit rather than treating each separately.
Procurement Checklist: Machine Stretch Film for AS/RS
- Confirm the load profiles that will actually be stored in the AS/RS: height, weight range, carton type, stacking pattern, and pallet footprint.
- Define stability requirements with the integrator: maximum acceleration and deceleration of the crane or shuttle, rack storage duration, and any inclination limits.
- Ask for containment force data, not only gauge and tensile values, and ask how the supplier’s recommended wrap pattern achieves it on loads like yours.
- Request tension retention behavior for storage periods matching your longest rack dwell time; the exact figure depends on conditions and should be confirmed with the supplier.
- Run a supervised trial with production loads, measuring containment force at three heights before and after a representative storage interval.
- Agree failure criteria and corrective actions with the automation integrator, so a wrap problem is caught before it becomes a rack jam or an unplanned outage.
Key Takeaways
- AS/RS handling removes the human tolerance that hides loose wraps in conventional warehouses; machine dynamics expose every weak band in the wrap.
- Containment force — uniform around and up the load — is the controlling metric, and it must be measured periodically, not assumed.
- Wrap geometry does half the work: anchor the load to the pallet, reinforce the top, stay inside the pallet footprint, and secure the film tail.
- Film choice matters most for long-term tension retention and puncture resistance; validate with trials on real production loads.
- Involve the AS/RS integrator when defining stability acceptance criteria, because machine dynamics determine what “stable enough” means.
FAQ
Why do loads shift in an AS/RS when the same loads were fine in a manual warehouse?
Automated stacker cranes and shuttles apply faster acceleration and deceleration than manual forklift handling, and they never slow down for a marginal load. A wrap that was “tight enough” under human handling fails under machine dynamics, especially at the top of the load where displacement is greatest.
Is a thicker film the best fix for load shifting?
Not necessarily. Containment force, wrap pattern, and anchoring control stability more than thickness alone. A properly applied high-performance downgauged film can outperform a heavier conventional film. The exact specification should be confirmed with the supplier against your load profile and machine.
How do I measure whether a wrapped load is stable enough for the rack?
Measure containment force at the base, middle, and upper third of the load, and run tilt testing to the inclination the load will experience in the automated path. Acceptance thresholds depend on your crane and shuttle dynamics, so agree them with the integrator rather than using a generic value.
What is the most commonly missed wrap defect in automated warehouses?
Film overhanging the pallet edge and loose film tails. Both are cosmetic issues in manual handling but cause rack jams, misaligned crane entry, and progressive unwinding in automated systems.
When should I consider stretch hood film instead of spiral wrapping?
Consider stretch hood when loads need the highest stability and weather protection, such as very tall or soft loads, or outdoor buffering before automated handling. It requires dedicated equipment, so it is usually evaluated at system design or major upgrade time.
Conclusion
Preventing load shifting in a high-bay AS/RS is a systems task: a film with the right retention and puncture behavior, a wrap pattern that anchors and reinforces the load where dynamics concentrate, machine settings verified by measured containment force, and acceptance criteria agreed with the automation integrator. Fixing any one element in isolation rarely stops the problem, because the failure modes interact.
If you are evaluating film for automated storage, share your load profiles — height, weight, carton construction, rack dwell time — and the handling dynamics of your crane or shuttle system. That information allows the wrap specification, containment force targets, and trial protocol to be built around your actual operation rather than assumptions.