

The difference between 5-layer and 7-layer machine stretch film comes down to control: a 7-layer co-extrusion line gives the formulator two additional layer positions, which enables asymmetric skins, dedicated specialty layers, and more downgauging headroom — while a quality 5-layer film fully covers most cartoned-goods, moderate pre-stretch applications at a lower cost. Layer count is a manufacturing architecture, not a quality grade; the resins and process control behind the layers decide how the film actually performs.
This article explains what co-extrusion does, how a 5-layer film is structured, what a 7-layer line adds, when each architecture is the smarter specification, and how to verify multi-layer claims with test data and wrapped-pallet trials before committing. It is written for packaging engineers, procurement teams, and converters evaluating machine stretch film specifications.
What Co-Extrusion Actually Does in Stretch Film Manufacturing
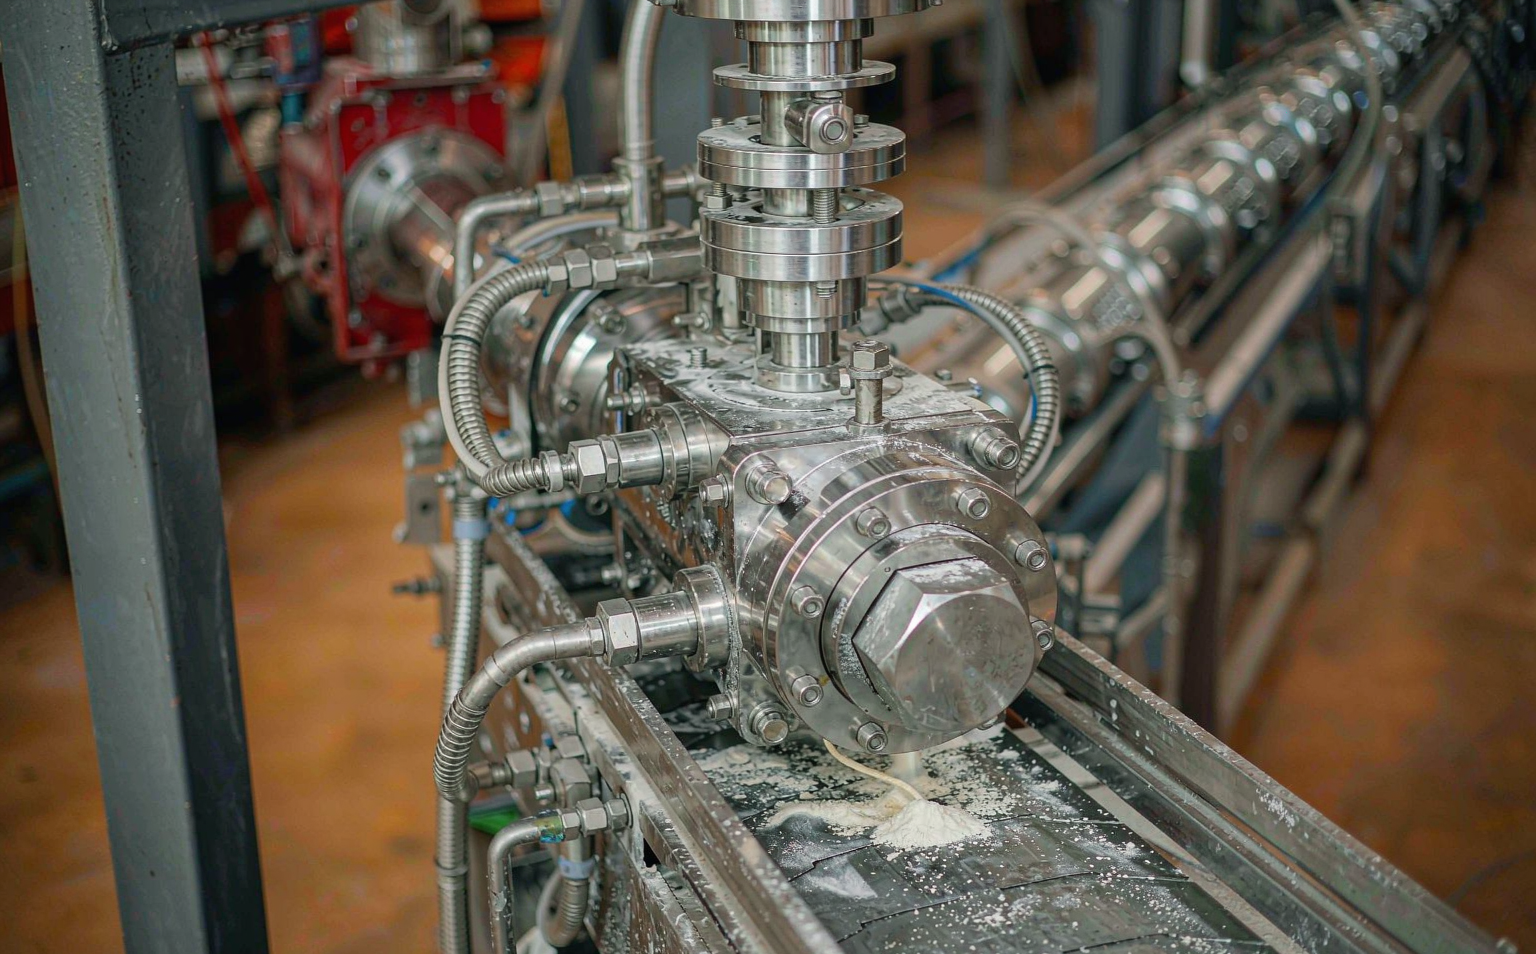
Multi-layer co-extrusion is the process of combining several molten polymer streams into a single film in one pass through a multi-manifold die, so that each layer is extruded simultaneously and fused before the film is quenched. Instead of laminating layers after the fact, the line builds the film from the inside out: an outer skin, one or more functional core layers, and an opposite outer skin, each tuned to a different job. No adhesives are involved, and the layers cannot delaminate in normal handling because they are bonded at the molecular level while molten.
The reason this matters for machine stretch film specifically is that no single polyethylene resin delivers everything a pallet load demands. A resin that resists puncture tends to stretch less before yielding; a resin with excellent elastic recovery is often softer and more vulnerable to tearing. Co-extrusion lets a manufacturer assign puncture resistance to the layers that face the load, cling to the outside layer that faces itself, and strength and recovery to the core — so the film behaves better than any of its individual components could.
The layer count is set by the die and feedblock design: a 5-layer line has five extruders feeding five layer positions, a 7-layer line has seven. When buyers compare the two, they are really comparing how many distinct jobs the film can be engineered to do at once, and how precisely each job can be isolated to the layer where it works best.
The Anatomy of a 5-Layer Machine Stretch Film
A conventional 5-layer machine film is laid out as skin / core / skin with intermediate tie or split-core layers between them. A typical functional split looks like this:
- Outer layers (both sides): a cling-containing or slip-tuned skin. One side carries the cling package so the film bonds to itself on the pallet; the other can be engineered for unwind behavior and abrasion resistance.
- Split core: the strength-bearing middle of the film. This is where higher-strength LLDPE — typically octene or metallocene-catalyzed grades on modern lines — delivers tensile strength, paglaban sa pagbutas, and elastic recovery.
- Intermediate layers: transition layers that let the skins and core bond cleanly and let the manufacturer fine-tune stiffness and elongation without disturbing the functional layers.
In practice, a well-designed 5-layer film covers the majority of machine-wrapping applications: general palletizing of cartoned goods, moderate pre-stretch ratios, and standard warehouse handling. It is the workhorse architecture of the industry, and for most buyers it is the correct one — more on that below.
What a 7-Layer Line Adds
A 7-layer architecture does not simply mean “more of the same plastic.” The additional layer positions give the formulator room to separate functions that a 5-layer film has to compromise on:
- Asymmetric layer design: with more positions, the outer layer that faces the pallet (the puncture side) and the outer layer that faces outward (the abrasion and cling side) can be built differently, each optimized for its own job rather than averaged between two.
- Dedicated barrier or specialty layers: a thin specialty layer — a high-tack resin, a strength layer, or a recycled-content layer in sustainable formulations — can be placed exactly where it is needed without diluting the strength core. This is also how post-consumer recycled content is incorporated while keeping food-contact or clean outer skins, which matters if your sustainability targets require PCR without performance loss.
- Downgauging headroom: more layers mean the strength distribution across the film cross-section can be modeled and balanced more precisely, which is what allows high-performance 7-layer films to be produced at lower gauges while holding puncture and tear targets. Whether a specific downgauge is achievable for your load profile should be confirmed with the supplier, because it depends on the line, the resins, and the application.
Think of it this way: 5 layers give the formulator five control knobs; 7 layers give seven. If your application only needs three knobs turned, the extra two are cost without benefit. If your application pushes the film hard — high pre-stretch, sharp-edged products, long storage, demanding sustainability specs — the extra control is exactly what you are buying.
5-Layer vs. 7-Layer: What Actually Changes for the Buyer
Layer count is a manufacturing architecture, not a quality grade. A first-class 5-layer film from a modern line will outperform a mediocre 7-layer film every time. The honest comparison is about what each architecture enables:
| Property | 5-Layer Film | 7-Layer Film |
|---|---|---|
| Puncture & tear resistance | Very good with quality resins; split core carries the load | Higher ceiling — strength layers can be placed and asymmetrically distributed for aggressive applications |
| Dart drop / impact | Good to very good depending on gauge and resin | Potentially higher at equal gauge, or equal performance at lower gauge |
| Layer customization | Skin/core/skin + intermediates | Asymmetric skins, dedicated specialty or PCR layers |
| Downgauging potential | Moderate | Higher — finer control of strength distribution across the cross-section |
| Typical cost position | Lower — simpler die, fewer extruders | Higher — more complex line and formulation |
| Best-fit applications | Cartoned goods, standard handling, moderate pre-stretch | Sharp/irregular loads, high pre-stretch, long storage, sustainability-driven specs |
Note what the table does not say: that 7-layer is always better, or that a specific puncture or tensile figure follows from layer count. Performance is set by the resin selection and process control behind the layers. When a supplier quotes layer count as if it were a performance guarantee, that is a signal to ask for the actual test data.
Where 7-Layer Architecture Pays For Itself
There are four situations where the 7-layer premium is usually money well spent:
- Sharp-edged and irregular loads. Unboxed product, cornered cartons, trays, and hardware punish film locally. A 7-layer film can place extra puncture resistance exactly where the film meets the load.
- High pre-stretch applications. Lines running 250–300% pre-stretch need film whose core survives that elongation without thinning into failure. The finer layer control of a 7-layer structure supports that. The exact pre-stretch ceiling for a given film should be confirmed with the supplier and validated on your machine before rollout.
- Downgauging and sustainability programs. If your target is fewer grams of film per pallet — or a defined percentage of PCR content without losing strength — 7-layer is the architecture that makes that a controlled engineering exercise rather than a gamble. Buyers procuring stretch film jumbo rolls for downstream converting should pay particular attention here, since the converting process adds its own demands on film consistency.
- Long dwell-time storage. Loads that sit in racking for months need elastic recovery that does not relax. Layer architecture that separates the recovery function from the cling function helps hold containment force over time.
When 5-Layer Film Is the Smarter Specification
For the other situations — and they are the majority — 5-layer is the rational choice. If your loads are stable cartoned goods, your pre-stretch is moderate, your storage windows are weeks rather than seasons, and your cost-per-pallet target is aggressive, the extra layers are architecture you will never use. Paying for seven knobs when three are turned is specification inflation.
There is also a procurement trap in the opposite direction: assuming layer count alone will fix a packaging problem. If film is failing on the line, the root cause is frequently machine setup — pre-stretch, tension profile, wrap pattern — or the wrong film type, not the film’s layer count. Diagnose the failure mode first, then choose the architecture.
How to Verify Multi-Layer Claims Before You Commit
Layer count cannot be seen with the naked eye on a finished roll, so verification comes down to documentation and testing:
- Ask for the test data, not the architecture. Dart drop, lakas ng makunat, elongation at break, puncture energy, at pagpapanatili ng pagkarga pagkatapos ng tinukoy na oras at temperatura — na may nakasaad na mga pamamaraan (ASTM D1709 para sa dart impact, ASTM D882 para sa makunat, ASTM D5458 o katumbas para sa pagbutas, halimbawa). Ang isang supplier na maaaring magpakita ng pare-parehong data sheet ay nagsasabi sa iyo ng higit sa isa na nagpapakita ng layer diagram.
- Magpatakbo ng isang side-by-side na pallet trial. I-wrap ang magkaparehong mga pallet sa kasalukuyang nanunungkulan na pelikula at ang kandidato sa parehong mga setting ng makina, sukatin ang lakas ng containment sa parehong taas, at suriin ang integridad ng pagkarga pagkatapos ng paghawak at pag-iimbak. Ang arkitektura ng layer ay hindi nakikita; ang pagganap ng wrapped-pallet ay hindi.
- Kumpirmahin ang gauge at yield. Walang kabuluhan ang price-per-roll nang walang na-verify na gauge; ihambing ang presyo sa bawat nakabalot na papag o bawat metro kuwadrado ng pelikula sa iyong aktwal na pre-stretch ratio.
- Itanong kung paano kumikilos ang pelikula sa iyong kagamitan. I-unwind ang mga kinakailangan sa pag-igting, pre-stretch compatibility, at ang antas ng pagkapit laban sa iyong mga roller ay dapat talakayin sa supplier — depende sa configuration ng makina, ang isang nominally superior na pelikula ay maaaring gumanap nang mas malala kung ito ay hindi tumutugma sa kagamitan.
Checklist ng Pagkuha: Multi-Layer Machine Stretch Film
- Failure mode ng kasalukuyang pelikula na naidokumento (mabutas, pagpapalaganap ng luha, pagkawala ng puwersa sa pagpigil, nakababa sa leeg?)
- I-load ang profile na nakasulat: timbang, taas, karton o hindi nakabalot, talim ng gilid, oras ng tirahan
- Nakasaad ang ratio ng machine pre-stretch at makakamit na mga target ng containment force
- Humingi ng ASTM ang supplier (o katumbas) pagsubok ng data na may mga pamamaraan, hindi lang layer count
- Ang pelikula ng kandidato ay naka-quote sa presyo sa bawat nakabalot na papag sa iyong gauge at pre-stretch
- Side-by-side na pallet trial ay sumang-ayon sa kasalukuyang nanunungkulan na pelikula, kasama ang isang tseke sa imbakan
- Kung umiiral ang mga target sa pagpapanatili: Porsyento ng nilalaman ng PCR at kung saan ito nakaupo sa istraktura ng layer
- Mga mamimili ng jumbo-roll: pag-convert ng compatibility at roll geometry na nakumpirma sa supplier
Mga Karaniwang Pagkakamali sa Pagbili sa Multi-Layer na Pelikula
- Ang pagbili ng layer ay binibilang bilang proxy para sa kalidad. Nangibabaw ang kalidad ng resin at kontrol sa proseso; Ang bilang ng layer ay nagtatakda lamang ng kisame sa kung ano ang magagawa ng formulator.
- I-upgrade ang pelikula bago suriin ang makina. marami “mga problema sa pelikula” ay mga problema sa pre-stretch o tension. Ayusin ang setup, pagkatapos ay muling suriin.
- Paghahambing ng mga rolyo sa halip na mga balot na papag. Dalawang pelikula sa magkaibang gauge at pre-stretch ratio ay maaaring magkaroon ng magkaparehong cost-per-roll at a 20%+ pagkakaiba sa cost-per-pallet.
- Nilaktawan ang pagsubok sa imbakan. Ang isang pelikulang may containment force sa unang araw at nakakapagpapahinga sa ikatlong linggo ay isang load-shifting claim na naghihintay na mangyari.
- Sobrang pagtukoy. Kung ang limang layer ay ganap na sumasakop sa aplikasyon, ang ikaanim at ikapito ay margin na ibinibigay mo sa supply chain.
Mga Pangunahing Takeaway
- Pinagsasama ng co-extrusion ang maraming polymer layer sa isang pelikula sa isang solong pass; bawat layer ay nakatalaga ng isang partikular na trabaho tulad ng puncture resistance, kumapit, o nababanat na pagbawi.
- 5-Ang layer film ay ang industriya ng workhorse at ang tamang detalye para sa karamihan ng mga cartoned-goods, katamtamang pre-stretch application.
- 7-ang layer film ay nagdaragdag ng asymmetric na disenyo ng layer, dedicated specialty layers, at higit pang downgauging headroom — mahalaga para sa matalim na pagkarga, high pre-stretch, long storage, at mga target na nilalaman ng PCR.
- Ang bilang ng layer ay arkitektura, not a quality grade: judge film sa pamamagitan ng ASTM-method test data at wrapped-pallet trials, hindi sa disenyo ng die.
- Ihambing ang mga pelikula sa presyo sa bawat nakabalot na papag sa iyong aktwal na sukat at pre-stretch ratio.
Mga Madalas Itanong
Lagi bang mas malakas ang 7-layer na stretch film kaysa sa 5-layer?
Hindi. Ang lakas ay nakasalalay sa pagpili ng dagta at kontrol sa proseso. Ang isang well-formulated 5-layer film ay higit na mahusay sa isang hindi maganda ang formulated 7-layer film. Ang ibinibigay ng 7-layer na arkitektura ay mas mataas kisame - higit pang mga posisyon upang ilagay ang lakas, mabutas, at mga espesyal na layer — na maaaring i-convert ng isang mahusay na formulator sa pagganap o mas mababang gauge.
Maaari bang paghiwalayin ang mga layer ng co-extruded stretch film?
Hindi sa ilalim ng normal na paghawak. Ang mga layer ay pinagsama habang natunaw sa loob ng die, hindi nakadikit pagkatapos, kaya walang malagkit na interface na mabibigo. Ang delamination ay nagpapahiwatig ng isang seryosong pagkakamali sa pagmamanupaktura, hindi pag-aari ng teknolohiya.
Alin ang mas mahusay para sa downgauging, 5-layer o 7-layer?
7-layer, pangkalahatan. Ang mas pinong kontrol sa distribusyon ng lakas sa kabuuan ng film cross-section ay ang nagbibigay-daan sa pagbawas ng gauge habang hawak ang pagbutas at pagkapunit ng performance. Kung gumagana ang isang partikular na downgauge para sa iyong mga load ay dapat kumpirmahin sa supplier at ma-validate sa isang pallet trial.
Paano ko susuriin ang multi-layer na claim ng isang supplier?
Humingi ng data ng pagsubok na may mga nakasaad na pamamaraan (halimbawa ASTM D1709 dart impact, ASTM D882 makunat), i-verify ang gauge at mag-iisa ang magbunga, at magpatakbo ng isang tabi-tabi na balot-pallet na paghahambing laban sa iyong nanunungkulan na pelikula sa magkatulad na mga setting ng makina.
Nakakaapekto ba sa presyo ang bilang ng layer?
Oo — ang 7-layer na linya ay may mas maraming extruder at mas kumplikadong die, kaya ang 7-layer na pelikula ay karaniwang nagdadala ng mas mataas na gastos sa produksyon. Ang trabaho ng mamimili ay suriin kung ang application ay talagang gumagamit ng karagdagang kakayahan; para sa maraming mga profile ng papag ito ay hindi.
Konklusyon
Ang pagpili sa pagitan ng 5-layer at 7-layer machine stretch film ay hindi isang tanong kung alin “mas mabuti” — ito ay isang tanong kung gaano karaming mga trabaho ang hinihiling ng iyong aplikasyon sa pelikula na gawin nang sabay-sabay. Matatag, karton, Ang mga katamtamang nakaunat na load ay ganap na inihahatid ng isang kalidad na 5-layer na pelikula. Mga produktong matalas ang talim, mataas na pre-stretch ratio, mahabang imbakan ng rack, agresibong downgauging, o PCR-content target ay kung saan ang 7-layer architecture ay kumikita ng premium nito. Sa bawat kaso, ang desisyon ay dapat nakasalalay sa data ng pagsubok na may mga nakasaad na pamamaraan at isang pagsubok na nakabalot sa papag, hindi kailanman sa layer count nag-iisa.
Kung tumitimbang ka ng 5-layer laban sa 7-layer na detalye — o magpapasya kung stretch hood film mas umaangkop sa iyong mga load na may mataas na katatagan kaysa sa spiral wrap — ipadala ang iyong mga profile ng load, mga setting ng pre-stretch, at mga target na cost-per-pallet, at ang istraktura ng pelikula, panukat, at ang pagsubok na protocol ay maaaring itayo sa paligid ng iyong operasyon sa halip na sa paligid ng isang generic na spec sheet.